As spillage accumulates below the system and clutters walkways, additional workers may be needed to clean it up, increasing labour costs and creating a potential workplace hazard. If it is not regularly addressed, spilled material can build up around the belt and tail pulley, fouling the unprotected return side of the belt.
By far the most expensive single component on any conveyor system, a belt with material adhered to its underside can suffer abrasion damage, mistracking and slippage, all of which increase power requirements.
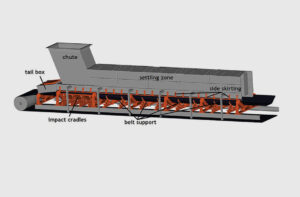
To avoid these consequences and minimise belt sag, conveyor designers recommend creating a sealed environment within the transfer chute. This can be achieved by reducing the distance between idlers or adding cradles.
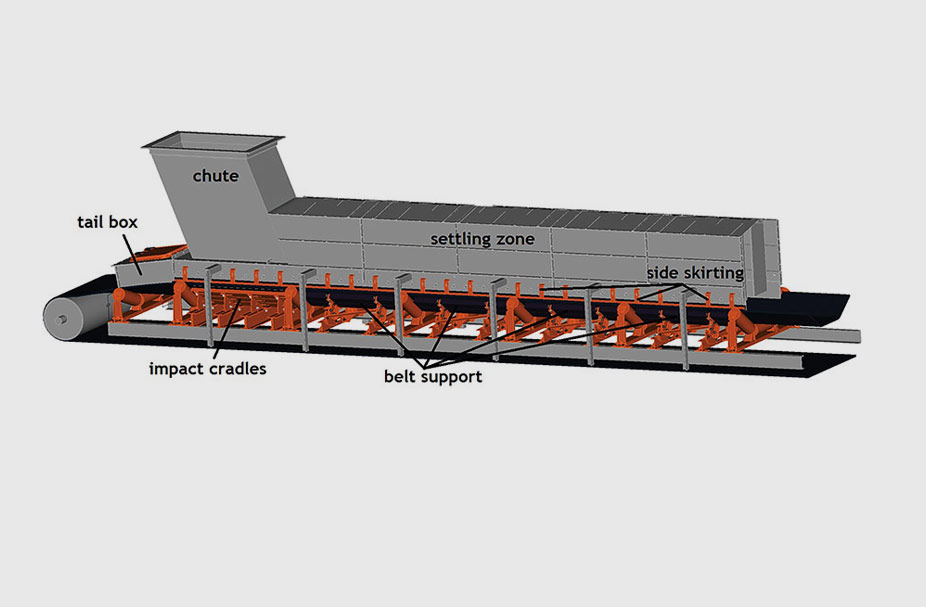
Cradles are durable urethane pads mounted on a rigid steel frame that create an even belt path, allowing the rubber skirting to maintain a tight seal along the entire length of the chute. The cradle/skirting combination not only eliminates gaps, but also provides greater airflow control through the loading, settling and stilling zones for improved dust and spillage suppression.
However, a tight seal can introduce additional friction. Although field tests have shown minimal erosion of the belting or splice, the added friction requires slightly more power, creating an ongoing cost that is an important consideration for operators. This article provides the calculations needed to determine the distance between idlers to reduce belt sag. It also explains how engineers can calculate the power requirements of a cradle system.
This data can help operators determine whether installing preventive measures – such as modern conveyor transfer point sealing equipment, including cradles and skirting – is more cost-effective over the long term than relying on reactive measures such as cleanup and ongoing equipment replacement.
Determining sag and idler distance
In Belt Conveyors for Bulk Materials, Sixth Edition, the Conveyor Equipment Manufacturer’s Association (CEMA) recommends limiting conveyor belt sag between idlers to 2% for 35-degree idlers and 3% for 20-degree idlers. The CEMA method is intended to limit sag outside the load zone and help prevent spillage.
To fully prevent spillage, dust, premature belt wear, wear-liner depreciation and skirt-seal wear in the load zone, sag must be significantly less than the levels recommended by CEMA. For example, using the CEMA method results in a recommended maximum sag between idlers of 12,5 mm for 35° idlers and 19 mm for 20° idlers.
For loading zones with multiple gaps and tonnes of material escaping from the chute, field tests have shown that this level of sag is clearly unacceptable for controlling fugitive materials in the load zone.
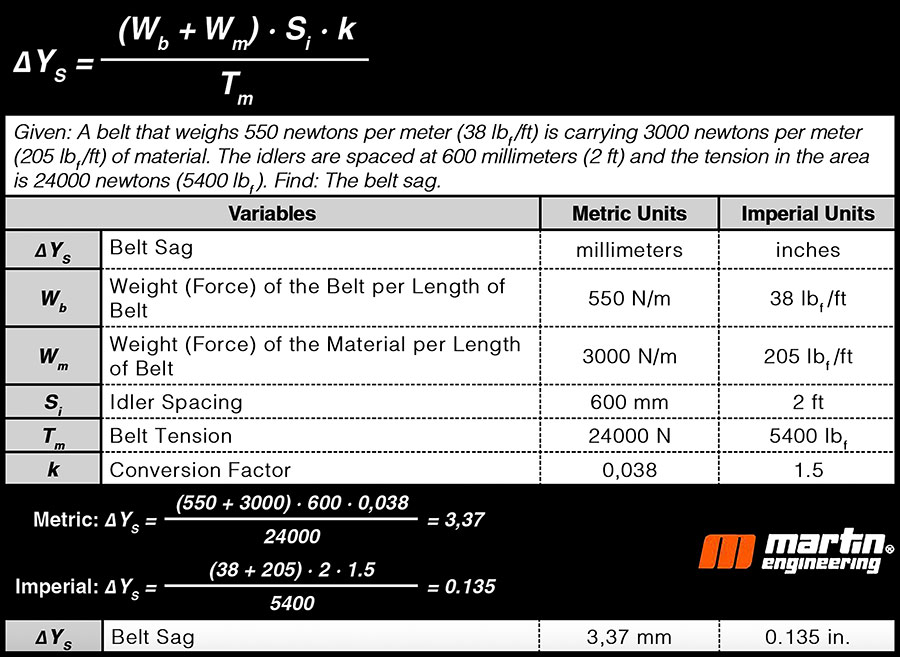
Sag (ΔYs) is proportional to the weight (force) of the belt and bulk material (Wb + Wm) and the idler spacing (SI), and it is inversely proportional to the minimum belt tension in the load zone (Tm). To control fugitive materials, designers should consider managing belt tension and idler spacing in the load zone to keep belt sag at no more than 3 mm, and preferably at 0.0. Even with very little sag, fugitive materials can escape and cause wear if belt support is not continuous.
For example, with an idler spacing of 600 mm, there is 3,37 mm of sag. If the idler spacing in the example is reduced to 178 mm, belt sag drops to 1 mm. On the other hand, when a belt-support system such as an impact cradle or air-supported conveyor section is used, idler spacing (SI) can be assumed to be 0.0. The calculation then yields belt sag of 0.0 because there should be no sag when the belt forms a continuous, flat surface.
Cradles and power requirements
Belt-support systems can have a significant effect on conveyor power requirements. Changes in belt support can have a particularly noticeable effect on short or under-powered systems. When calculating the theoretical power requirements of proposed changes to belt-support systems, conveyor designers should ensure that adequate drive power is available to compensate for the additional friction placed on the conveyor.
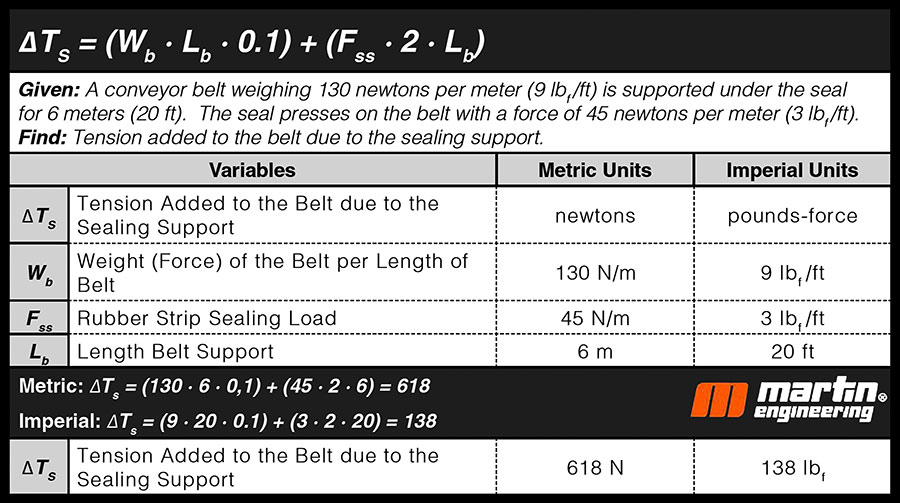
Added kilowatt (hp) consumption can be calculated by determining the additional belt tension using the standard methods recommended by CEMA. The coefficient of friction of the new or proposed support system, multiplied by the load placed on the belt support from belt weight, material load and the sealing system, equals the added tension.
There is no need to account for the removal of idlers, the incline of the conveyor or other possible factors, as estimates produced by this method will, in most cases, be higher than the power consumption experienced during actual operation. In applications where a lubricant, such as water, is consistently present, actual power requirements may be one-half, or even less, than the amount estimated through these calculations.
Conclusion
Additional power requirements and costs may seem minor when compared with the power consumed by operating with one “frozen” idler or several idlers affected by material accumulation. By implementing the proper belt-support systems, a plant can prevent the more costly problems that arise when fugitive material escapes from the transfer point.
Cleanup of spillage not only increases labour costs but, in lieu of unscheduled downtime, can expose workers to activities around and beneath a running conveyor – a major cause of injuries and fatalities in the bulk-handling industries.
Testing has found that a well-designed system accepts the slightly higher power consumption required to prevent spillage rather than incur the much higher power consumption and greater consequences associated with fugitive material. The costs of installing and operating proper belt-support systems represent an investment in ongoing efficiency and workplace safety.